Sorry, no sales person is available right now to take your call. Pls leave a message and we will reply to you via email as soon as possible.
Kinji Group | Full Process Analysis of 6-Layer RO4350B+IT180A High-Frequency Hybrid Laminate Board
2026-08-28
What Challenges Does RF PCB Face in the 5G Massive MIMO Era?
Moving from Sub-6GHz to millimeter-wave bands, the number of RF channels in 5G base stations has surged from 4T4R to 64T64R and even 128T128R. Under the Massive MIMO architecture, the AAU (Active Antenna Unit) integrates PA power amplifiers, LNA low-noise amplifiers, RF transceiver circuits, and antenna feed networks on a single board, which simultaneously carries multi-gigahertz RF signals and a large number of digital control signals.
This imposes a seemingly contradictory requirement on PCB substrate materials: RF channels demand extremely low dielectric loss and stable dielectric constant, while digital control layers require high Tg, high heat resistance, and cost-effectiveness. A full high-frequency solution delivers excellent performance but at prohibitive cost, while a full FR-4 solution suffers from severe loss degradation above 3GHz. High-frequency hybrid laminate boards emerged precisely in this context and have become the mainstream architecture for 5G RF boards.
Why Choose "Hybrid Laminate"? – The Optimal Engineering Balance of Performance and Cost
The core logic of hybrid laminates is zone-based material selection: RF signal layers are placed on low-Dk, low-Df high-frequency substrates, while power layers, ground layers, and digital signal layers use high-Tg FR-4 materials, achieving synergistic integration of both materials through a single lamination process.
Taking a 6-layer hybrid board as an example, a typical stack-up strategy is as follows:
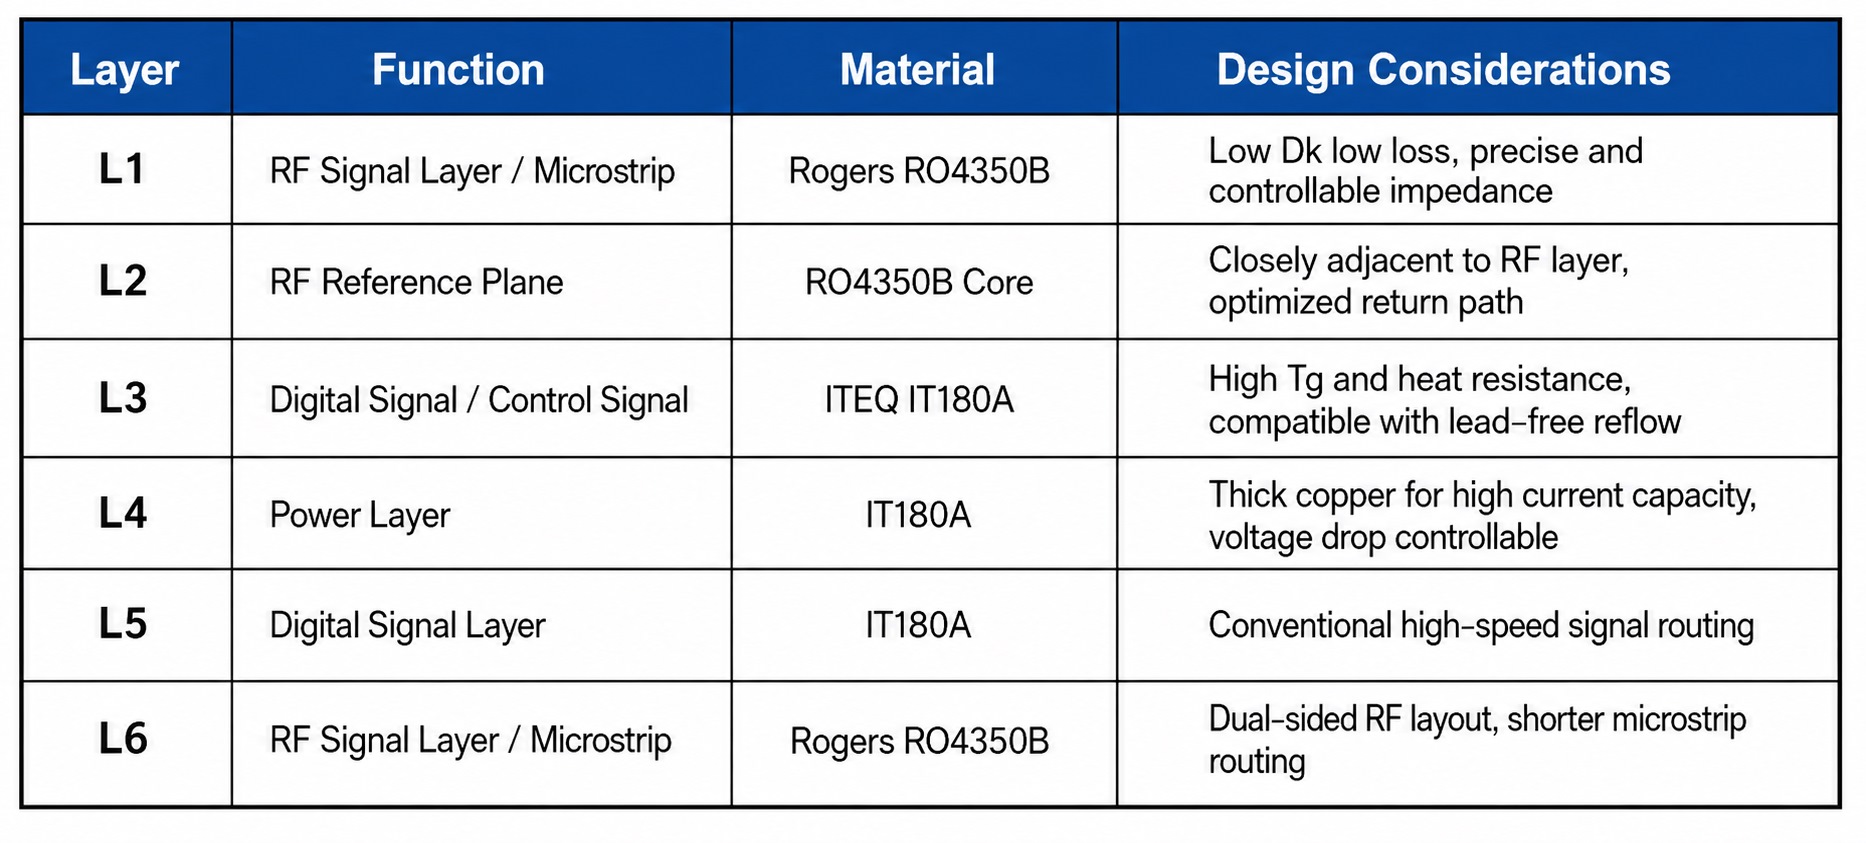
The direct benefits of this architecture are: RF performance approaching that of full high-frequency boards, material cost reduction of 30%–50%, while retaining the high reliability and standard processing compatibility of FR-4 layers.
In-Depth Material Selection Analysis: The Synergistic Logic of RO4350B and IT180A
RF Layer Substrate: Rogers RO4350B
RO4350B is a ceramic-filled hydrocarbon laminate from Rogers Corporation for the commercial RF market. Key electrical parameters are as follows:
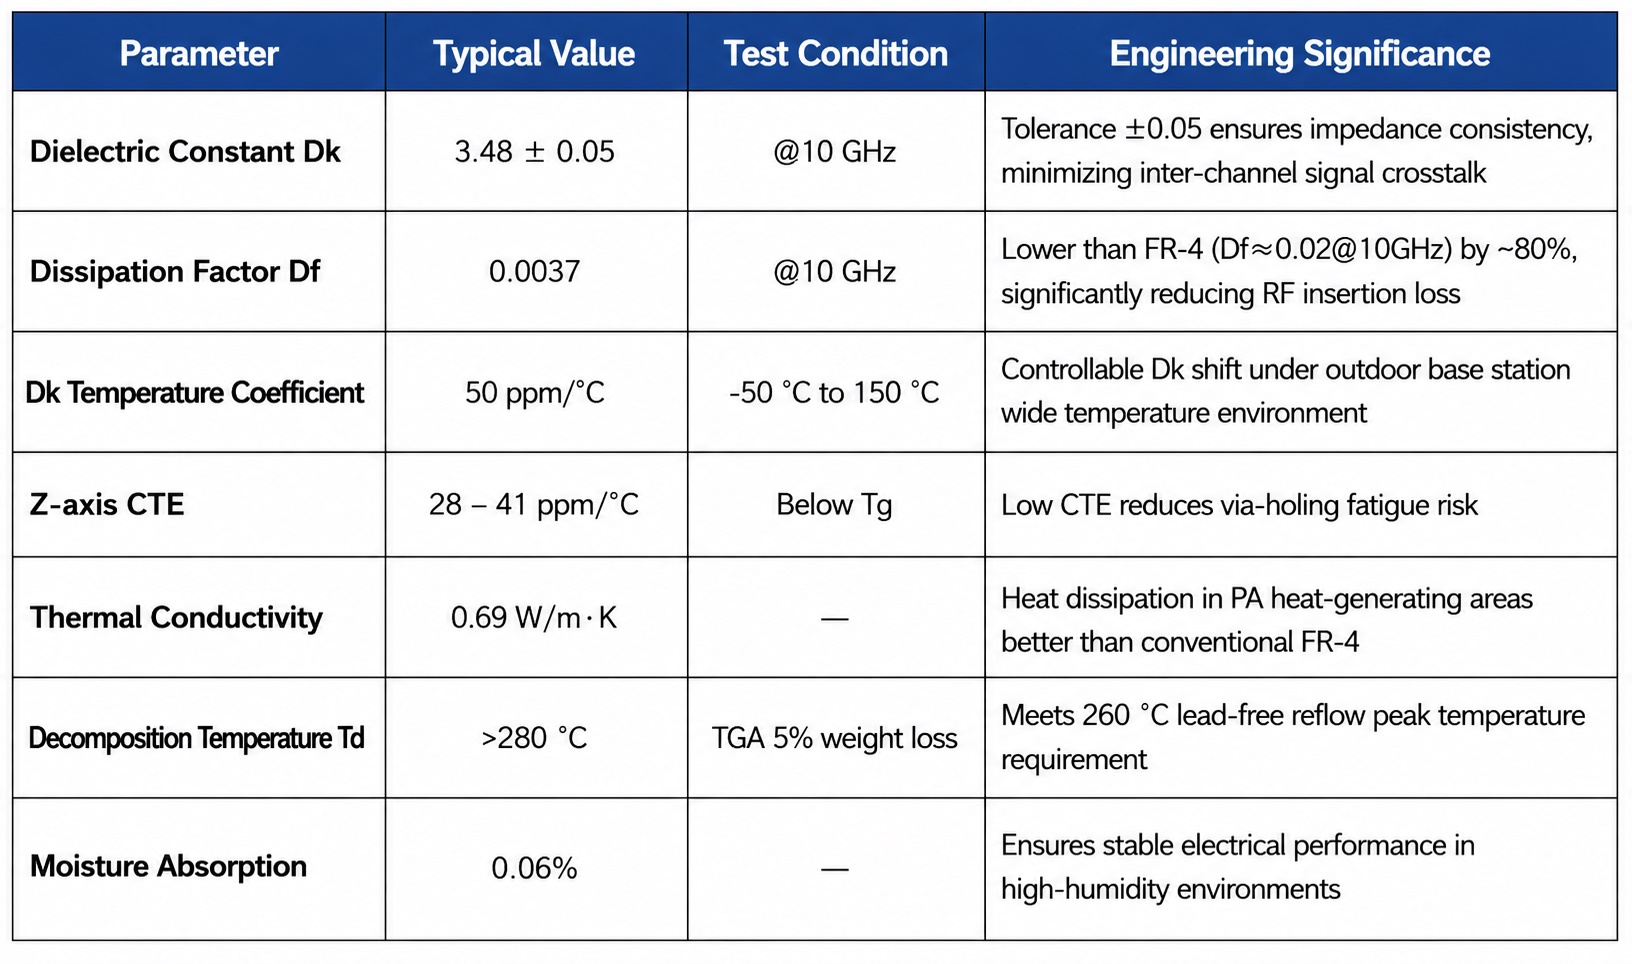
The core advantage of RO4350B lies in its processing compatibility: unlike pure PTFE substrates that require plasma treatment and special bonding sheets, RO4350B can be processed using standard epoxy/glass fabric routes. Drilling, copper plating, and lamination can all be completed on conventional PCB production lines. This is the key reason it has become the de facto standard for 5G base station RF boards.
Digital/Power Layer Substrate: IT180A from Iteq
IT180A is a high-Tg (175°C–180°C) multifunctional filled epoxy substrate positioned as a high-reliability upgrade to FR-4:
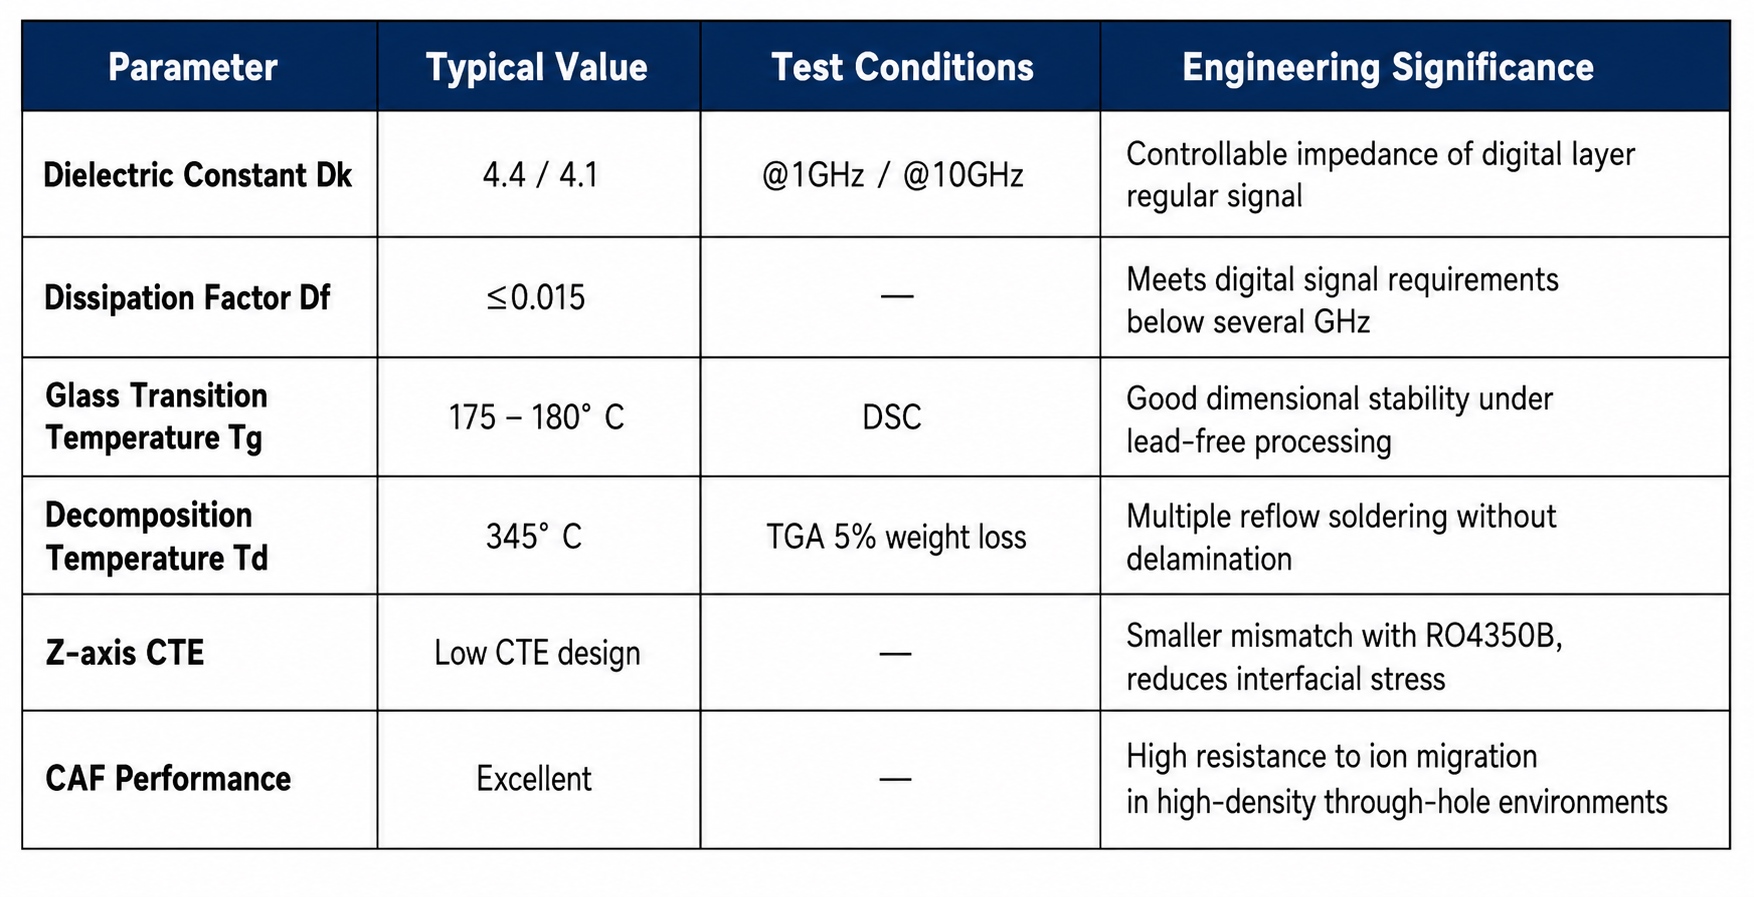
The selection logic for IT180A lies in balancing heat resistance and CAF resistance: 5G AAU boards typically adopt high-density designs with 0.4mm minimum via diameter and 4/4mil line width/spacing. With dense vias and elevated operating temperatures, IT180A's low CTE and high Td effectively suppress CAF (Conductive Anodic Filament) growth and via copper cracking risks.
Key Process Parameters and Engineering Implementation for 6-Layer Hybrid Boards
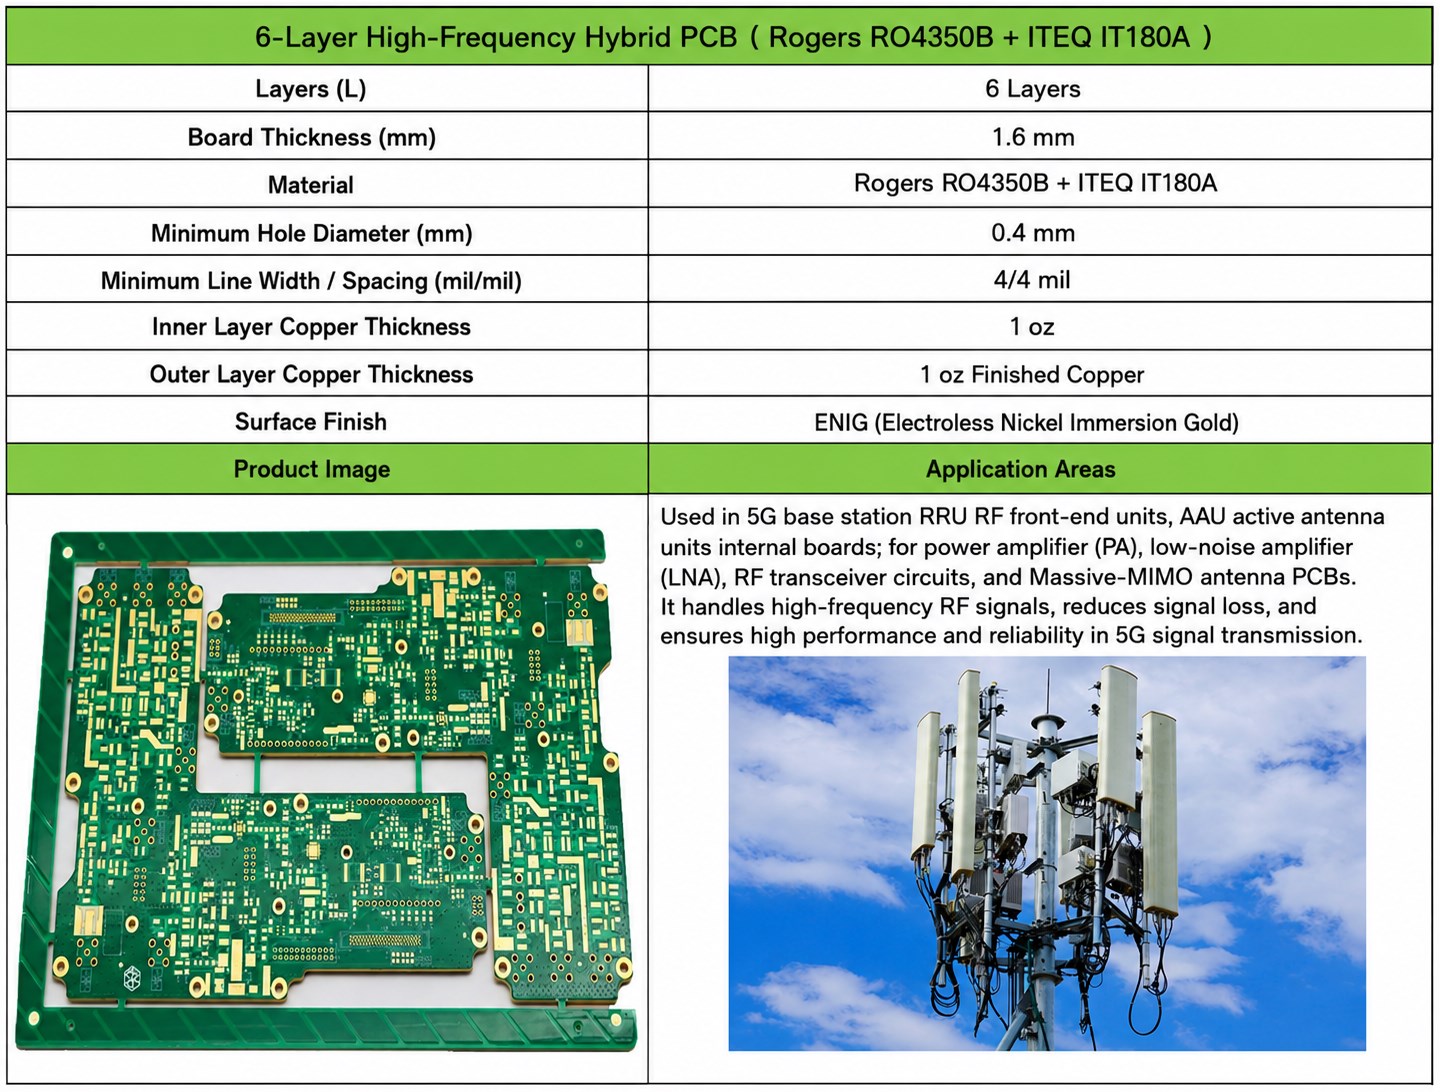
Taking a 6-layer high-frequency hybrid board in mass production at Kinji Group as an example, core manufacturing parameters are as follows:
Impedance Control: Standard Formulas Won't Suffice
Impedance calculation for hybrid boards is the first engineering hurdle. Because RO4350B (Dk=3.48) and IT180A (Dk=4.1@10GHz) have different dielectric constants, and the equivalent dielectric thickness may slightly shift due to prepreg flow during lamination, directly applying conventional impedance models often results in measured values deviating by more than ±10% from design targets.
Standard engineering practices:
· Use field solvers (e.g., Polar Si8000/9000) for stack-up modeling, inputting Dk and Df values for both materials separately;
· RF microstrip lines must reference a complete ground plane of the same material, avoiding cross-material reference;
· Perform first-article impedance testing before full lamination, and fine-tune line width compensation based on measured values;
· Extract impedance coupons from each batch in production, controlling within ±10% (and ±7% for critical RF lines).
Lamination Process: CTE Mismatch Is the Root Cause of Delamination
The most critical challenge in hybrid lamination is the difference in Z-axis CTE between the two substrates. RO4350B has a Z-axis CTE of approximately 28–41 ppm/°C, while conventional FR-4 is around 50–70 ppm/°C. During lamination heating to 180°C and subsequent reflow soldering peaks at 260°C, interfacial shear stress can exceed 12 MPa—if not properly controlled, this directly leads to delamination or uneven prepreg flow.
Kinji Group's production engineering employs the following combined approach:
① Symmetric Stack-up Design
The 6-layer board uses a symmetric "HF-FR4-FR4-HF" structure, with L1/L6 as RO4350B and L3/L4/L5 as IT180A, with matching prepreg (PP) transition layers in between. This ensures that thermal expansion forces from top and bottom counteract each other, controlling warpage within 0.75%.
② Controlled Lamination Profile
· Ramp rate: 2–3°C/min (lower than the 4–5°C/min for conventional FR-4) to reduce internal stress from asynchronous heating of the two materials;
· Soak stage: 120°C–140°C for 20–30 minutes to allow full PP flow and outgassing of volatiles;
· Cure stage: 180°C–185°C for 60–90 minutes to ensure complete curing of the IT180A system;
· Cooling stage: controlled at 2–3°C/min to avoid stress concentration at the interface from rapid cooling.
The above parameters are based on the actual process window of Kinji Group's 6-layer hybrid board production line; adjustments may be needed according to press model and PP batch.
③ Interfacial Bonding Material Selection
Between RO4350B and FR-4, it is recommended to use low-flow prepreg or Rogers' dedicated bonding sheets (such as 4450F) to strictly control resin flow and prevent excessive squeeze of the high-frequency layer resin, which could cause Dk shift.
Drilling and Via Metallization: Managing Smear at the Bimaterial Interface
Hybrid board drilling faces the challenge of different cutting characteristics between the two materials: RO4350B resin is relatively soft and prone to smear adhesion on hole walls, while IT180A fillers are hard and cause greater drill bit wear. For 0.4mm small-diameter vias, inadequate smear removal leads to poor copper adhesion and even voids in the hole wall.
Standard process path:
· Drill bit selection: Use 130°–140° drill point angle UC (Under Cut) drills to reduce entry burrs;
· Feed parameters: Reduce feed speed appropriately (10–15μm/rev) for the RO4350B layer, while allowing higher feed for the IT180A layer;
· Smear removal: Use plasma cleaning + chemical micro-etching combined process on the RO4350B side, and conventional potassium permanganate desmear on the IT180A side;
· Via copper thickness: Electroless copper deposition + electrolytic copper plating, average thickness ≥25μm, meeting IPC Class 3 requirements.
Through segmented feed and combined plasma cleaning processes for 0.4mm vias in hybrid boards, Kinji Group consistently achieves via copper adhesion exceeding IPC Class 3 standards, with production yield above 98%.
Dimensional Control: Managing the "Individuality" of High-Frequency Materials
The X/Y axis dimensional characteristics of RO4350B differ from those of FR-4. After multilayer lamination, without proper expansion/contraction compensation, inner-layer patterns may misalign with drilling. Engineering practice requires measuring the expansion coefficients of each inner-layer core before lamination, and applying differentiated compensation in the drilling program to ensure layer-to-layer registration accuracy within ±0.075mm.
Typical 5G RF Application Scenarios
This 6-layer RO4350B+IT180A hybrid board is highly focused on 5G base station RF front-end applications. Kinji Group's product has been mass-delivered to multiple communications equipment manufacturers for RRU and AAU products, covering PA/LNA boards and Massive MIMO feed networks in the Sub-6GHz band.
RRU (Remote Radio Unit) / AAU (Active Antenna Unit) Internal Boards
RRUs and AAUs are the RF cores of 5G base stations. Their internal boards must simultaneously handle RF signals from transceivers and digital control signals. The hybrid architecture places PA output matching networks and LNA input matching networks on RO4350B layers, while ADC/DAC interfaces, power management, and control buses are placed on IT180A layers, achieving optimal balance between RF performance and system integration.
PA Power Amplifiers and LNA Low-Noise Amplifiers
PA output signals can reach watts to tens of watts and are sensitive to dielectric loss and thermal conductivity; LNA inputs demand extremely low noise figures, where dielectric loss directly impacts the overall system noise figure. RO4350B's Df=0.0037@10GHz ensures low insertion loss in RF channels, and its thermal conductivity of 0.69 W/m·K effectively aids heat dissipation in PA areas.
Massive MIMO Antenna RF Feed Boards
In 64T64R and larger arrays, the antenna feed network contains numerous microstrip lines, power dividers, and couplers, where line width/spacing precision directly affects array amplitude and phase consistency. The 4/4mil fine-line capability combined with RO4350B's stable Dk ensures phase consistency and cross-polarization discrimination (XPD) across large arrays.
Selection Recommendations and Engineering Tips
For hardware teams evaluating 5G RF board solutions, the following recommendations are worth noting:
· Not all high-frequency layers need RO4350B: Signal layers operating below 3GHz can consider high-speed FR-4 materials like IT180A for further cost optimization;
· Ensure complete RF reference ground: Avoid splitting the ground plane beneath RF microstrip lines, which would cause impedance discontinuities and radiation degradation;
· ENIG surface finish is preferable to OSP: For RF contact points subject to repeated insertion/removal or soldering, the contact resistance stability of ENIG is superior to that of organic solderability preservatives;
· First-article validation is indispensable: Impedance, warpage, and via reliability must be fully verified in the first-article stage; it is recommended to complete -40°C to +85°C temperature cycling tests (≥100 cycles) before mass production;
· Choose manufacturers with proven hybrid production experience: Hybrid process yield heavily depends on the production line's accumulated experience with lamination profiles, drilling parameters, and impedance compensation. Prioritize PCB suppliers with proven 5G RF board delivery records.
In the high-frequency hybrid board domain, Kinji Group has established end-to-end capabilities from material selection and stack-up design to lamination processes. The 6-layer RO4350B+IT180A hybrid board is in stable mass production, serving multiple communications equipment manufacturers' 5G RF board projects. For R&D teams with high-frequency hybrid requirements, it is recommended to involve the manufacturer early in the solution stage for stack-up reviews, proactively mitigating impedance deviation, warpage, and delamination risks from a manufacturability perspective.
Conclusion
The complexity of 5G RF front-ends continues to rise—from Sub-6GHz toward millimeter-wave evolution, and from 64T64R toward even larger array expansions. Demands on PCB substrates and processes will only grow more stringent. High-frequency hybrid laminates, as a mature and mass-production-validated architecture, will remain the mainstream choice for 5G RF boards for a considerable period. A deep understanding of RO4350B and IT180A material properties, along with precise control of key hybrid process parameters, is essential knowledge for every RF hardware engineer and PCB process engineer. Kinji Group will continue to deepen its expertise in high-frequency hybrid technology, delivering reliable and efficient PCB solutions for 5G and next-generation communications equipment.
trending news
Contact Us