Sorry, no sales person is available right now to take your call. Pls leave a message and we will reply to you via email as soon as possible.
From FPC to CCS Integrated Cover Plate in New Energy Battery Packs: Core Concepts, Mainstream Processes, and Technology Trends
2026-10-20
In the power battery packs of new energy vehicles, CCS (Cell Contact System) and FPC (Flexible Printed Circuit) are two core components, respectively undertaking the key functions of signal acquisition and power transmission. To facilitate understanding, the battery pack can be compared to the human body: FPC is like the "sensory nerves" covering each cell, collecting voltage and temperature data in real time; CCS is an integrated "functional module" that combines acquisition nerves, power transmission channels, and insulation protection. The two have clear divisions of labor and deep collaboration, jointly forming the underlying sensing and control network of the battery management system (BMS), and providing fundamental guarantees for the safe and stable operation of the battery pack.

I. Analysis of the Core Concepts of CCS and FPC
(1) CCS Integrated Busbar (Cell Contact System)
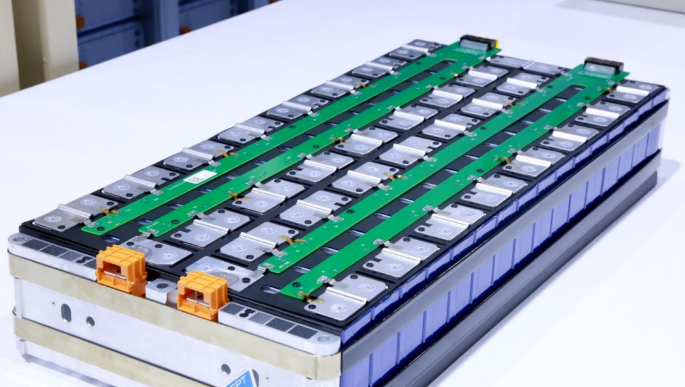
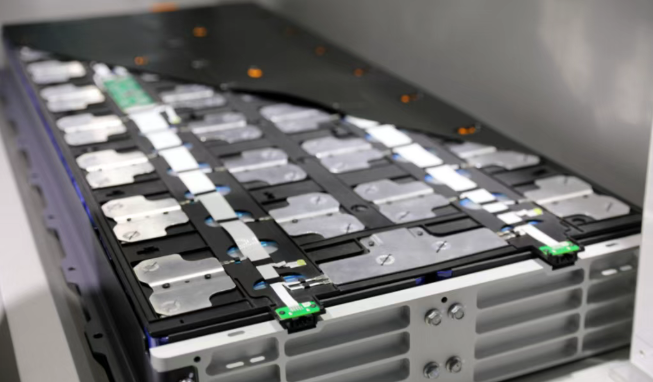
CCS (Cell Contact System), commonly known in the industry as integrated busbar or battery cover plate assembly, is a highly integrated core functional component in power battery modules. It integrates multiple functions such as high-voltage electrical connection, cell signal acquisition, structural support and positioning, and electrical insulation protection, comprehensively replacing the traditional decentralized "wire harness + bracket" structure.

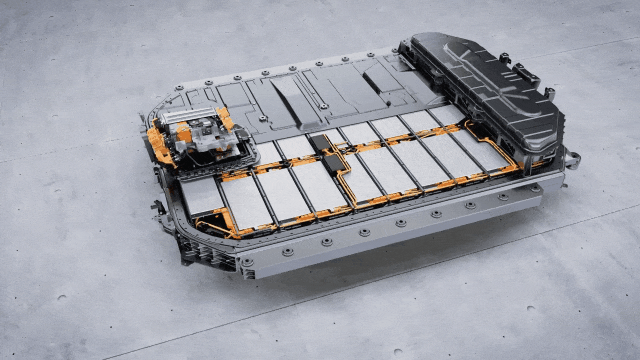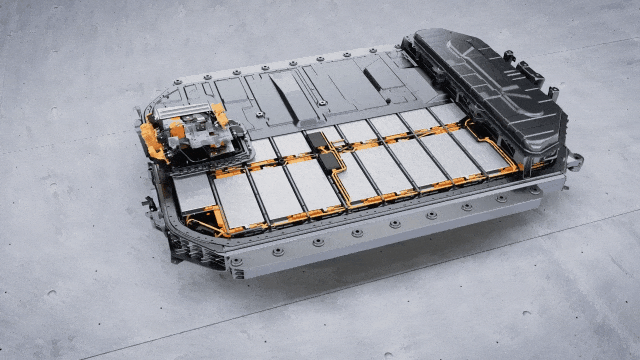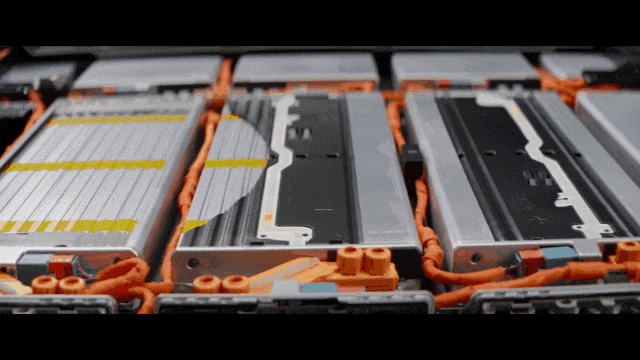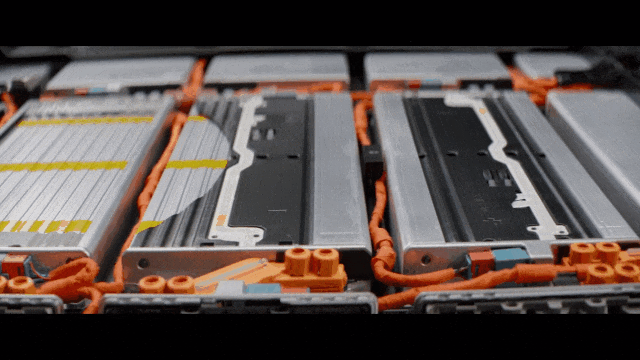
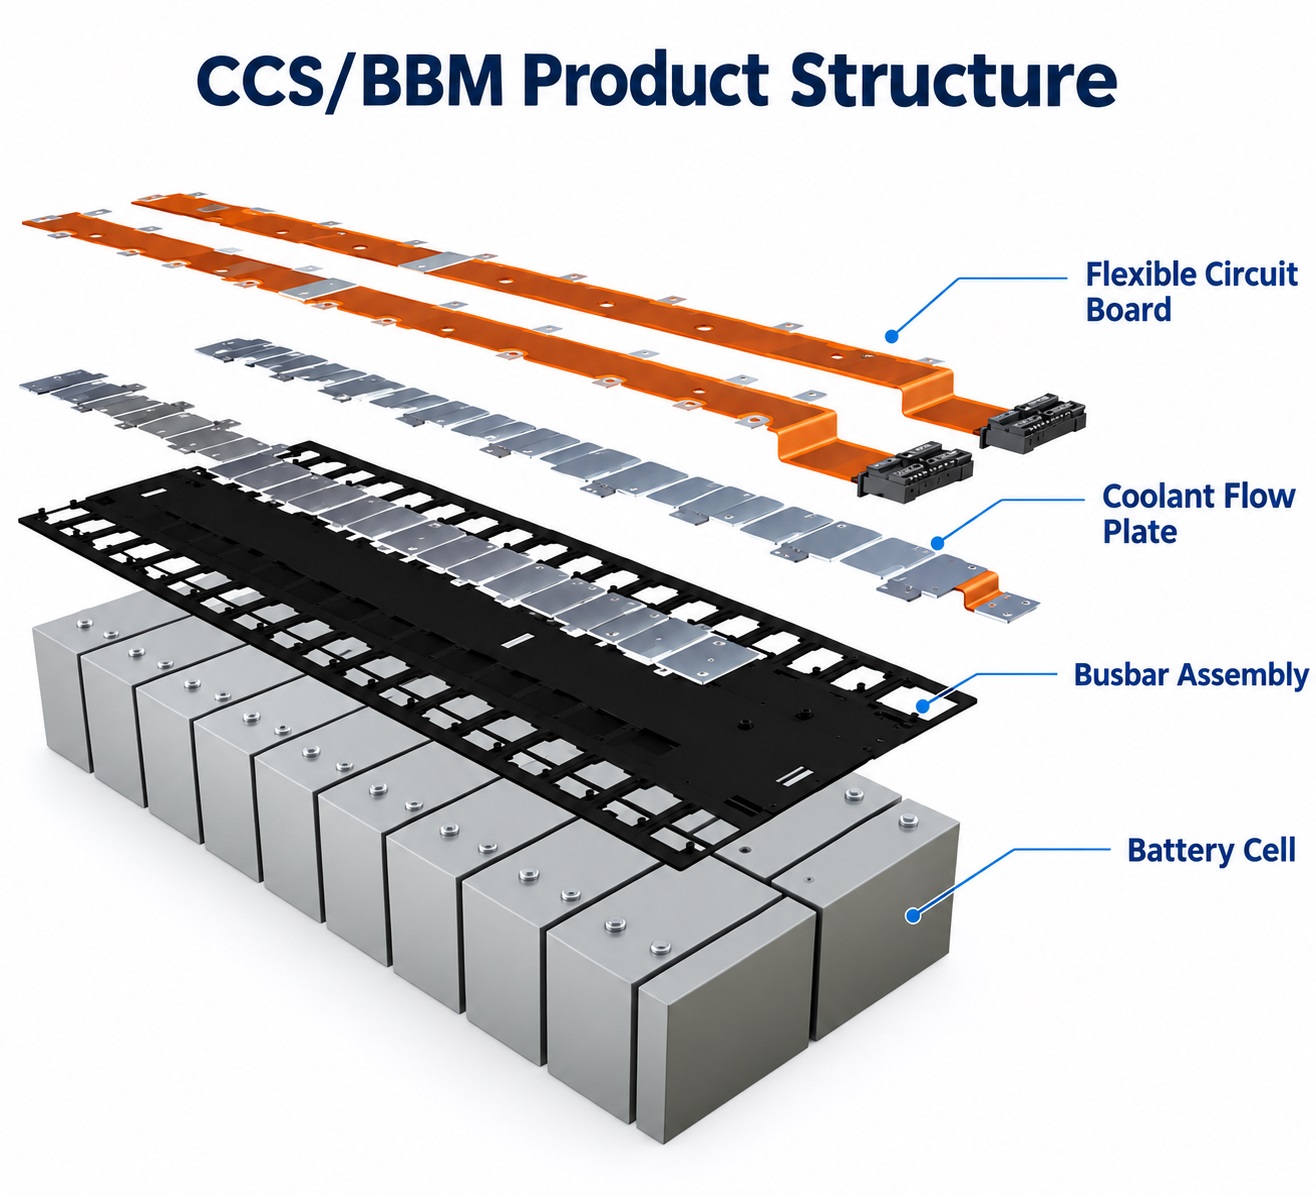
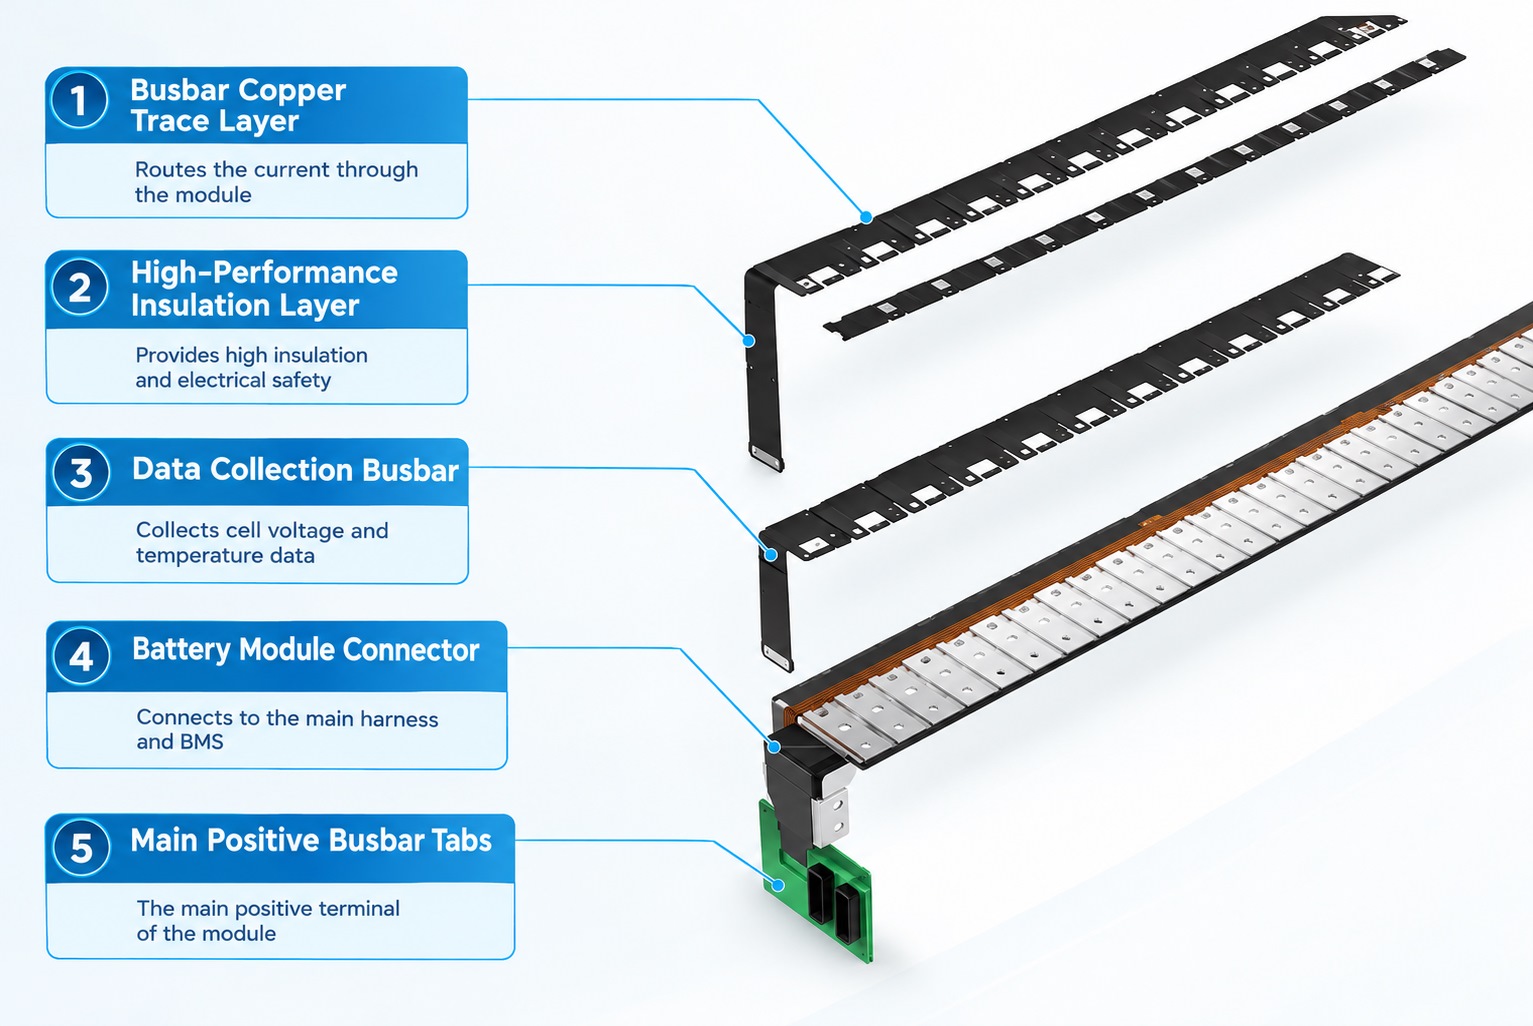
A standard CCS assembly consists of three core units:
· Signal acquisition unit: with FPC as the core carrier, responsible for precise acquisition and low-loss transmission of cell voltage and temperature signals;
· Plastic structural unit: provides overall structural support, insulation isolation, and positioning and fixation;
· Conductive current-carrying unit: composed of copper busbars and aluminum busbars (copper bars, aluminum bars), carrying large currents and realizing series-parallel networking between cells.
The core functions of CCS cover three aspects:
① Build a high-voltage power supply circuit through metal conductive bars to realize series-parallel connection of cells;
② Accurately collect the voltage and temperature signals of each cell and upload them to the BMS, providing data support for state estimation, balancing control, and overheating protection;
③ Some integrated CCS integrate fuse protection structures, which can provide passive protection against overcurrent and overheating, enhancing system safety redundancy.
(2) Flexible Printed Circuit
FPC (Flexible Printed Circuit) uses polyimide (PI) or polyester film (PET) as flexible substrate, and is manufactured through precision etching, surface mounting, lamination, and other processes, featuring bendability. In the CCS system, FPC serves as the core carrier for signal acquisition. The circuit integrates components such as NTC temperature sensors and acquisition nickel sheets, corresponding one by one to individual cells, achieving high-precision, low-loss signal acquisition and transmission.
The conventional thickness of FPC is only 0.1–0.3 mm. It has outstanding advantages such as being ultra-thin and lightweight, arbitrarily bendable, highly integrated in circuitry, and neatly routed, highly matching the development trend of compactness and high integration in power battery packs.

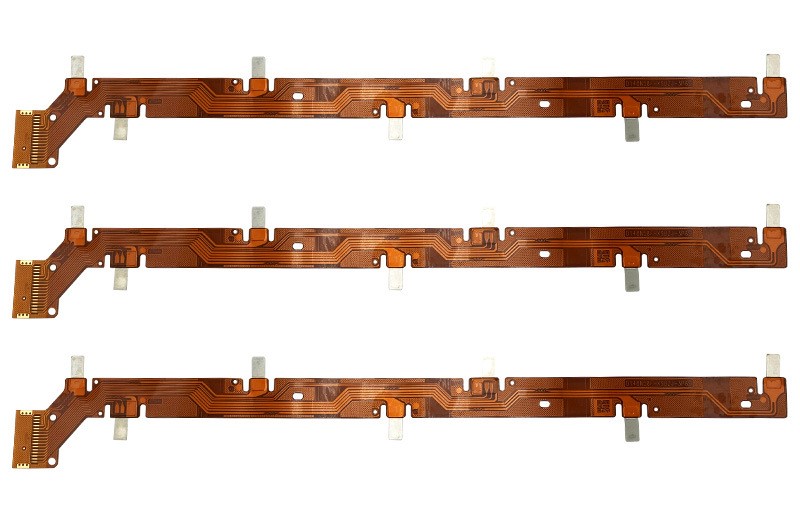
The collaboration among the three can be concisely summarized as:
FPC — the "nerves" of perception, responsible for signal acquisition;
Copper/aluminum conductive bars — the "blood vessels" of power transmission, undertaking large-current transmission;
Plastic bracket — the "skeleton" of support, realizing structural shaping and insulation protection.
The three are integrated into one, forming a fully functional and structurally compact CCS assembly module.
II. Core Value of CCS in Power Battery Packs
Before 2022, domestic power battery packs generally adopted traditional discrete copper wire harness acquisition solutions, namely the "single wire harness corresponding to single electrode" mode. As the number of cells surged, system integration increased, and acquisition accuracy requirements rose, the drawbacks of this solution became increasingly prominent: complicated wiring harnesses occupying large space; assembly highly dependent on manual labor with low automation and limited production efficiency; numerous contact points with high risk of poor contact and signal failure, making quality consistency difficult to guarantee; and relatively high overall weight, unfavorable for vehicle lightweighting.
The large-scale application of CCS integrated busbars has completely revolutionized the structural design and production assembly mode of battery packs. It integrates dispersed acquisition wire harnesses, insulating brackets, conductive bars, and components into an all-in-one modular assembly, with significant core advantages:
· Greatly simplifying the number of parts, reducing structural thickness, and simplifying assembly processes;
· Adapting to automated assembly line operations, reducing manual intervention, and significantly improving production efficiency and product consistency;
· Outstanding lightweighting effect: mainstream FPC-CCS solutions can replace dozens of traditional wire harnesses per module, achieving weight reduction of several kilograms at the module level.
At present, the market penetration rate of FPC-based CCS has exceeded 60%, becoming the mainstream supporting solution for power battery packs in new energy passenger vehicles.
III. Mainstream CCS Process Types and Core Characteristics
The industry adopts a standardized two-dimensional classification for CCS technical solutions: by type of signal acquisition component, and by overall forming manufacturing process. Each solution presents clear differences in structural form, physical performance, production cost, and application scenarios.
(1) Classification by Signal Acquisition Component
1. FPC Solution (Industry Mainstream)
Current market share exceeds 60%. The standard structure is: FPC flexible circuit + acquisition nickel sheet + copper/aluminum conductive bar + blister board/PET film hot-press integration.
Advantages: ultra-thin and lightweight (substrate thickness only 0.1–0.3 mm), extremely high space utilization; circuit integrally etched and formed with few solder joints, excellent reliability and stability; flexible and bendable, able to adapt to slight expansion deformation during cell charge-discharge cycles; suitable for fully automated mass production with stable yield.
Limitations: high-end FPC substrates and supporting equipment require large investment, and processing is complex; FPC only handles signal acquisition and has no large-current carrying capacity, so it must be used with metal conductive bars.
2. PCB Solution
Made with FR4 epoxy resin rigid substrate. The standard structure is: PCB rigid board + acquisition nickel sheet + aluminum conductive bar + blister heat riveting/PET film hot-press fixation.
Advantages: mature process, extremely low production cost, and low quality control difficulty; rigid substrate with high flatness and dimensional stability, not easy to deform, suitable for standardized mass production.
Limitations: substrate thickness reaches 1–2 mm, structurally heavy, and poor lightweighting effect; rigid and non-bendable, unable to adapt to cell cyclic expansion and contraction, prone to stress cracking and abnormal signal acquisition during long-term use, with limited application scenarios.

3. FFC Solution
Using PET as insulating substrate, formed by lamination of tinned copper wire and insulating layer, it is a simplified flexible signal transmission component.
Advantages: excellent flexibility, capable of 180° folding and bending, suitable for complex and narrow assembly spaces; good anti-electromagnetic interference performance, no dedicated mold required, high automated lamination production efficiency, and short delivery cycle.
Limitations: limited voltage withstand level, insulation performance requires additional reinforcement; relatively low circuit integration, difficult to meet the high-end module requirements of high-density cell arrangement.

4. FDC Solution
Using PI/PET film as substrate, directly formed by rotary die-cutting process, eliminating traditional etching procedures, it is a highly cost-effective alternative solution.
Advantages: outstanding cost advantage, capable of reducing production cost by more than 30% compared with FPC solution, suitable for large-size, standardized mass-production modules.
Limitations: limited processing precision, minimum line width/line spacing ≥0.25 mm, unable to meet the high-precision acquisition requirements of small-spacing, high-density cells, and not suitable for high-end precision scenarios.

(2) Classification by Overall Manufacturing Process
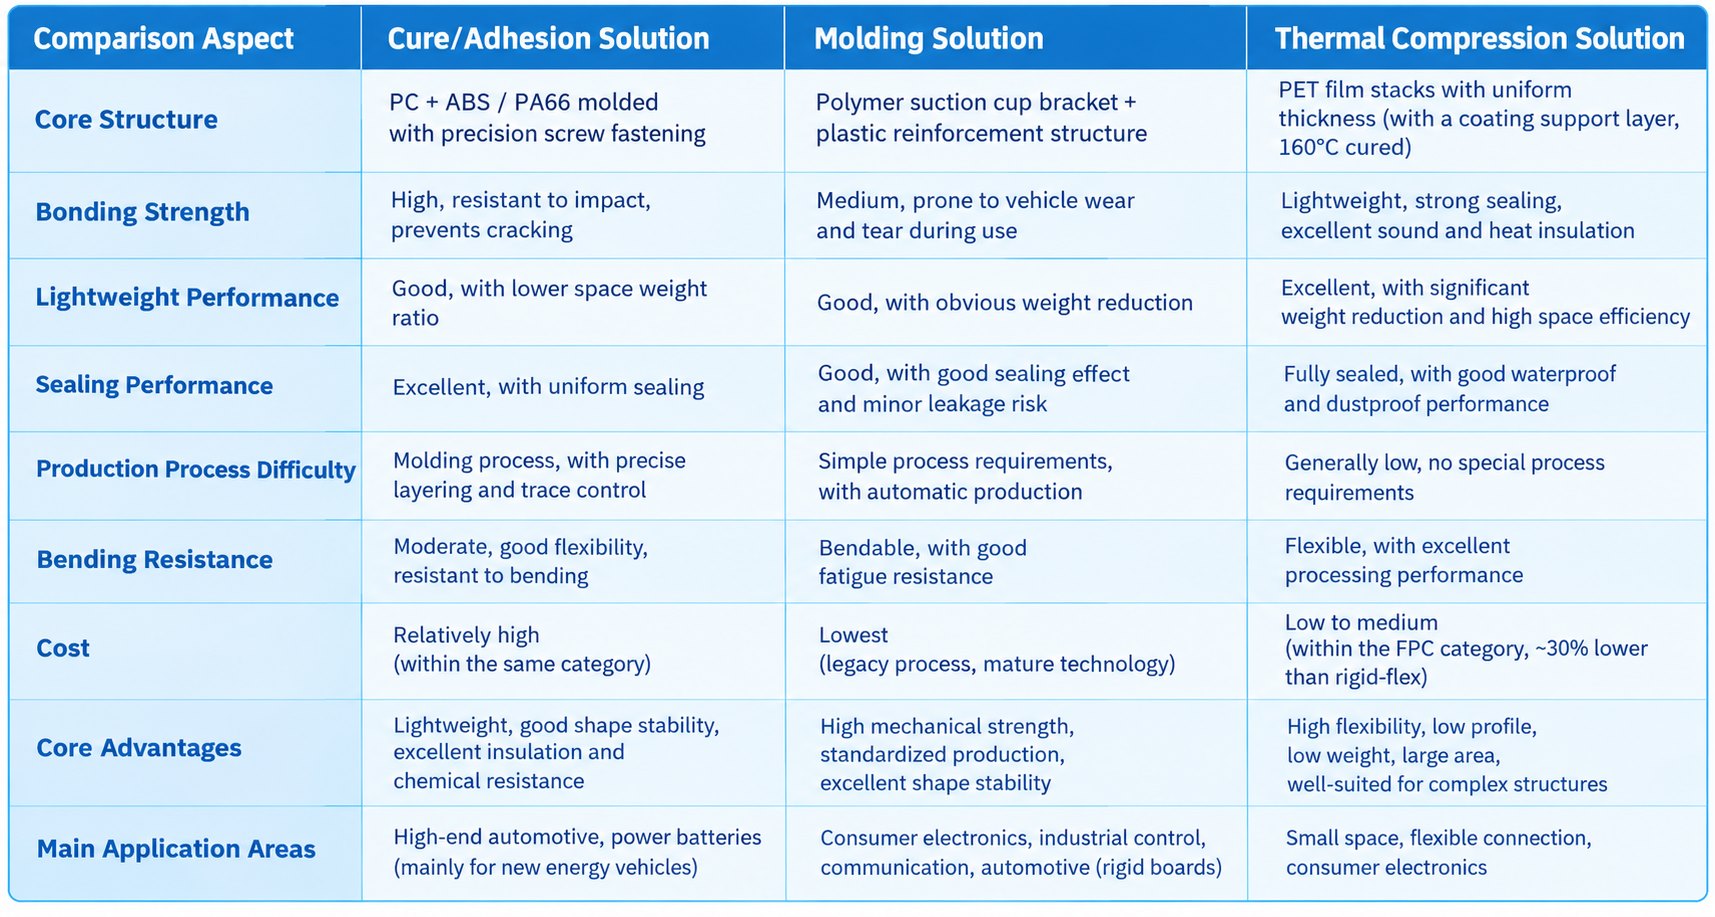
1. Injection Molded Tray Solution
The earliest process to achieve large-scale industrial application in the industry. It uses flame-retardant engineering plastics such as PC+ABS and PA66, forms an integrated rigid tray as the structural skeleton through high-temperature injection molding, and then fixes and assembles conductive bars and acquisition components.
Advantages: high structural strength, excellent vibration and impact resistance, strong insulation reliability, suitable for fixed energy storage, large power batteries, and other high-safety-requirement scenarios.
Limitations: large tray wall thickness, overall heavy, poor lightweighting and space utilization, difficult to adapt to the lightweight and thin-profile needs of passenger vehicles.
2. Blister Heat Riveting Solution
A lightweight iteration of the injection molding process. It uses thin-wall blister-formed brackets to replace heavy injection-molded trays, and then uses high-temperature heat riveting to melt and fasten FPC/PCB acquisition components, conductive bars, and brackets.
Advantages: greatly reduced wall thickness, achieving lightweight and thin-type upgrading; raw material and production costs lower than injection molding, with high cost-effectiveness; flexible structural adaptation, compatible with multiple specifications of cell modules.
Limitations: mechanical strength of thin-wall structure inferior to injection-molded trays, vibration and impact resistance somewhat weakened, not suitable for extreme bumpy working conditions.
3. Hot-Press Film Solution
The fastest-iterating advanced process in recent years and the one with the highest adaptability for passenger vehicles. It eliminates the solid plastic bracket and uses high-strength PET insulating film as the carrier. Multiple layers of materials such as signal acquisition components, conductive bars, and insulating film are precisely stacked and positioned, and then cured in one step under constant temperature and pressure of about 160 °C, forming an ultra-thin integrated CCS assembly.
Advantages: extremely thin and lightweight structure, industry-leading integration, maximizing the release of internal space in the battery pack; fully sealed lamination with excellent dustproof, waterproof, and leakage-proof performance; high standardization, suitable for fully automated mass production, and excellent product consistency.
Limitations: large investment in dedicated hot-press equipment, relatively long curing cycle per batch, and comprehensive production cost higher than injection molding and blister processes.
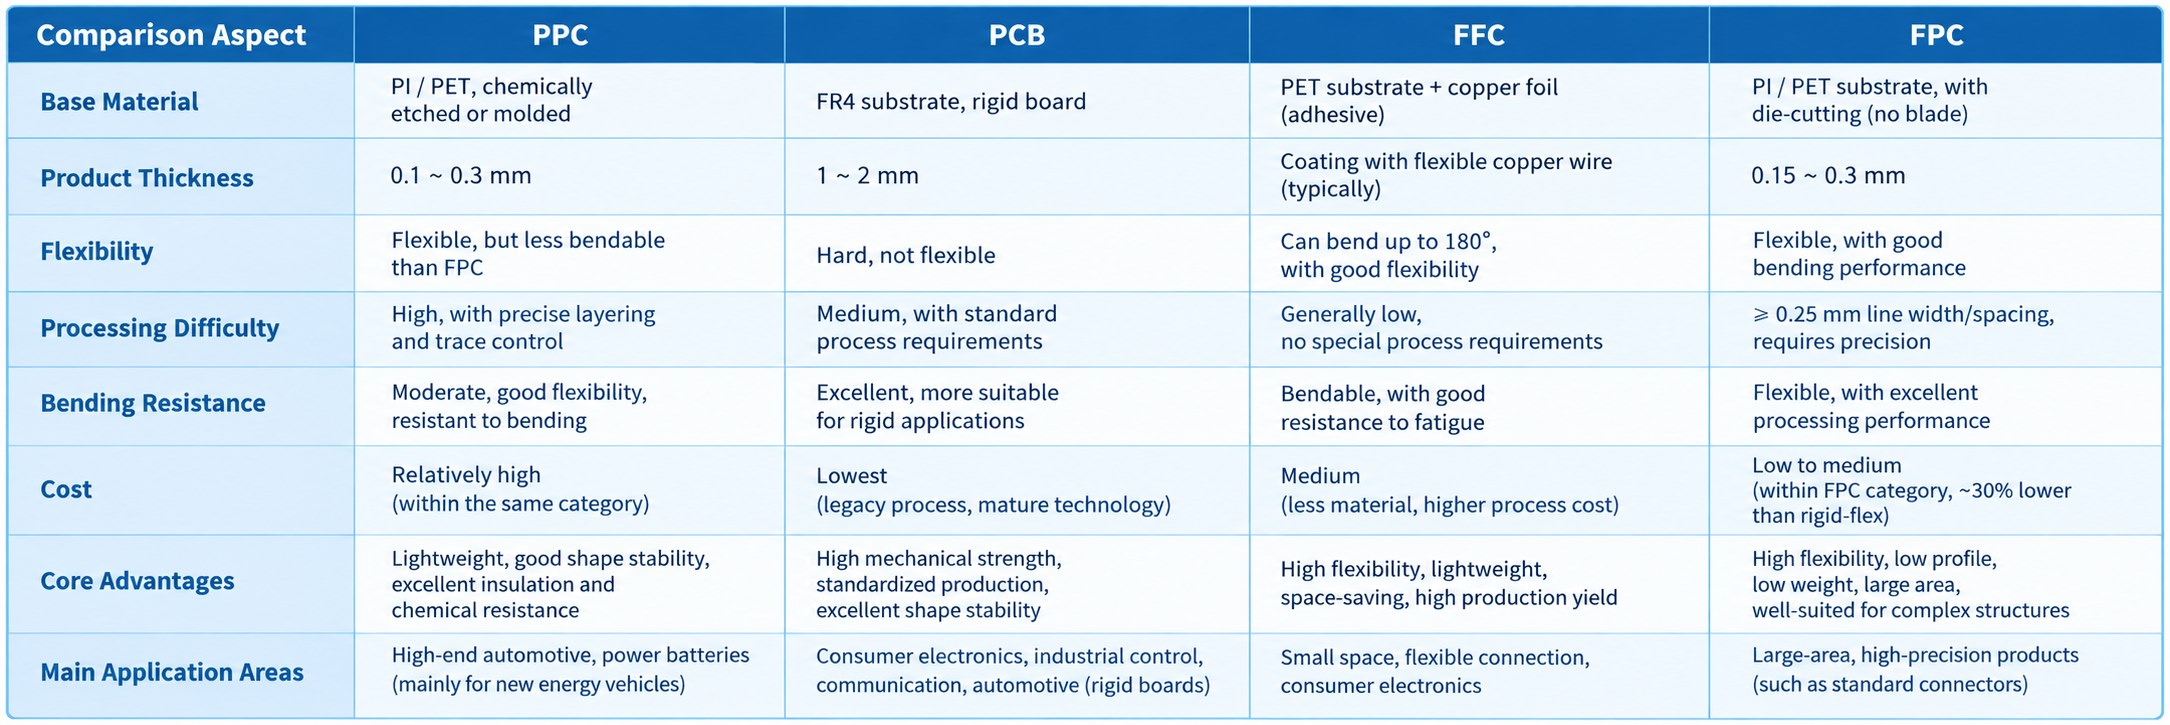
IV. Summary Table of Mainstream CCS Process Parameter Comparison
(1) Comparison by Signal Acquisition Component Process

(2) Comparison by Overall Manufacturing Process

V. Summary of Technical Iteration and Industry Development Trends
Looking at the technological evolution path of CCS integrated cover plates, the industry has always iterated around five major directions: thinness and lightweighting, high integration, high reliability, automated mass production, and low cost. The technical route has achieved a clear leap from traditional discrete wire harnesses → injection-molded bracket CCS → lightweight blister heat-riveting CCS → mainstream FPC + hot-press film integrated CCS.
At present, the combination of FPC flexible acquisition + PET hot-press film, with its ultra-thin and lightweight structure, high reliability, high space utilization, and excellent mass-production consistency, has become the optimal mainstream solution for power battery packs in passenger vehicles. At the same time, emerging acquisition solutions such as FFC and FDC, relying on differentiated cost advantages, are gradually being implemented in scenarios such as energy storage batteries, commercial vehicle power batteries, and standardized modules, forming an industry pattern of differentiated competition among multiple technical routes.
For practitioners in battery pack design, R&D, and manufacturing, accurately mastering the performance advantages and disadvantages, cost differences, and scenario adaptability of various CCS processes is key to reasonably balancing safety, performance, and cost in product development, and is also an important foundation for achieving battery system structural optimization and enhancing product market competitiveness.

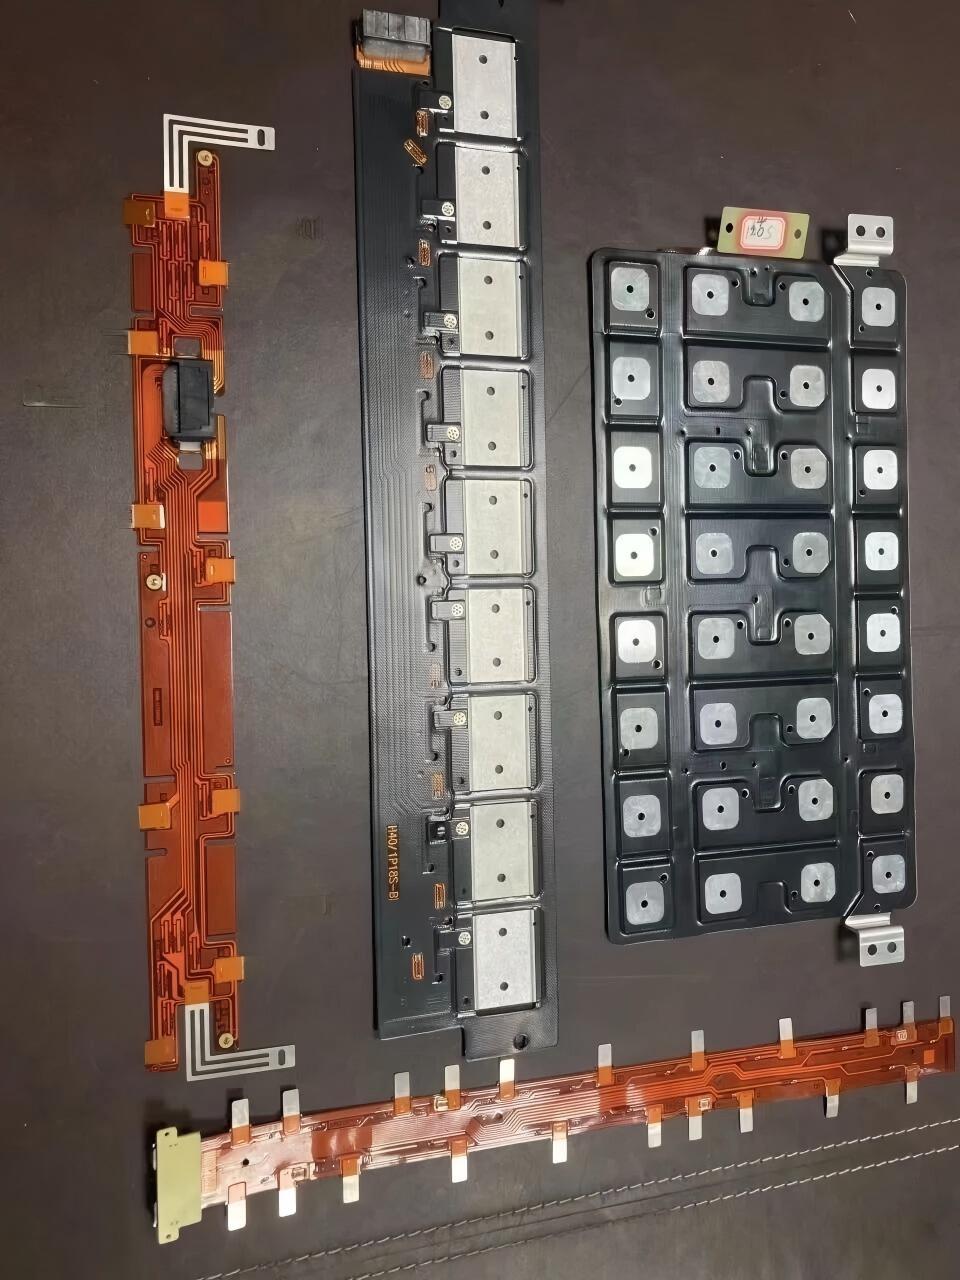
KINJI GROUP New Energy Battery Pack CCS Products
trending news
Contact Us