Sorry, no sales person is available right now to take your call. Pls leave a message and we will reply to you via email as soon as possible.
In-Depth Analysis of Core Technical Challenges in Ceramic Metallization
2026-09-07
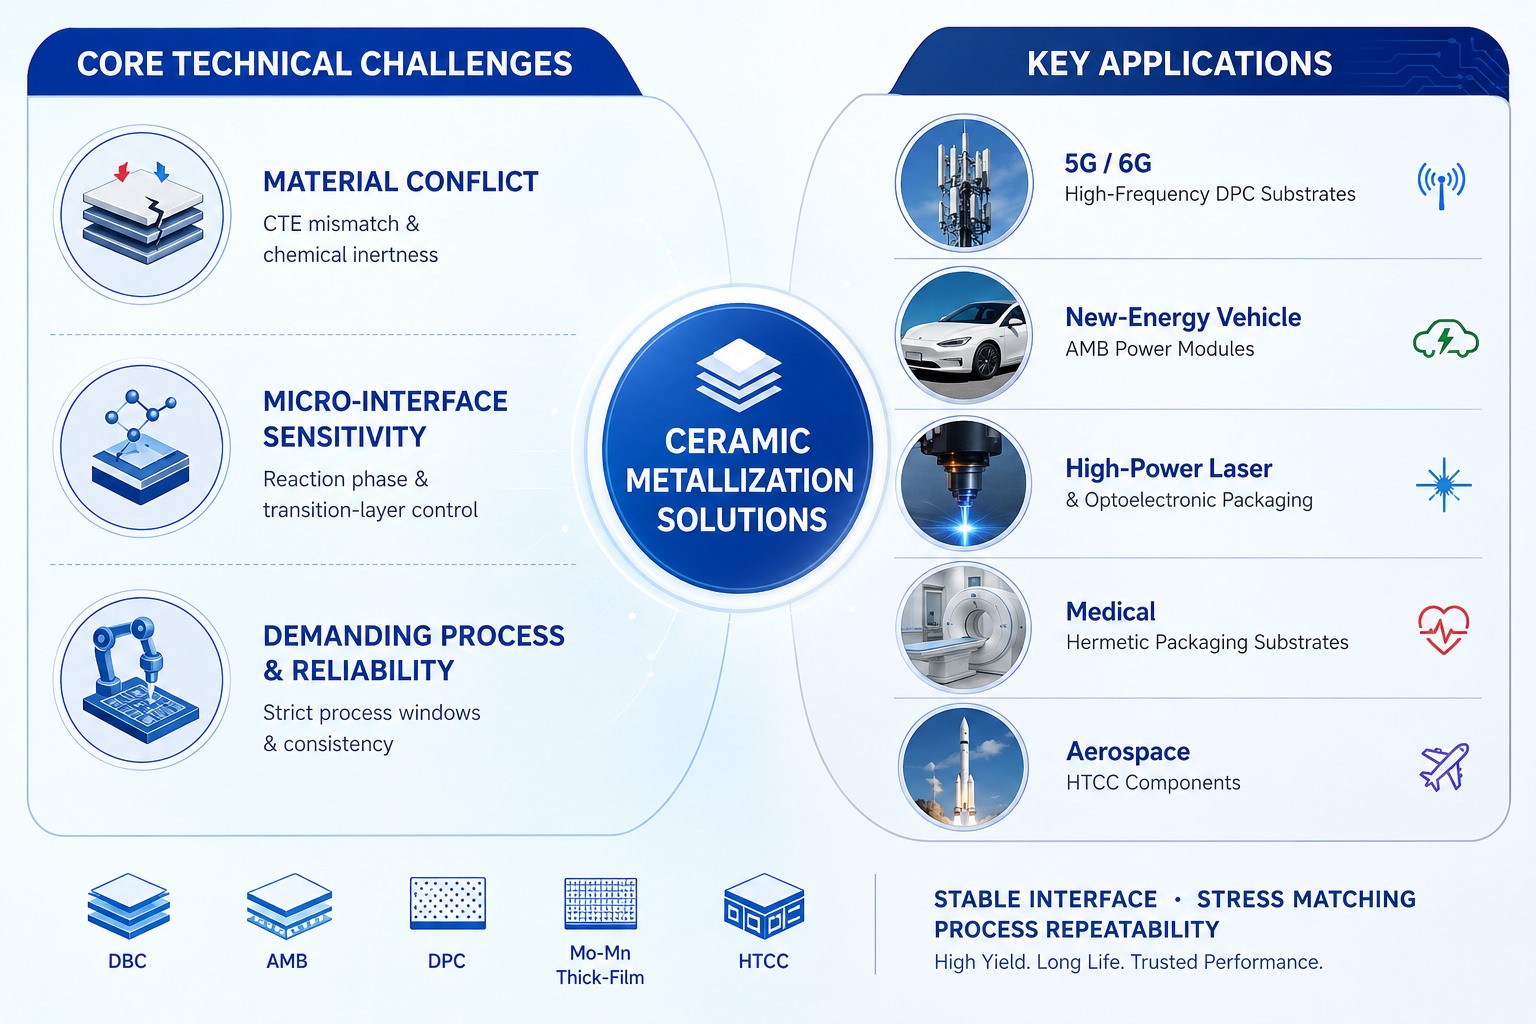
Ceramic substrates, with their high thermal conductivity, excellent electrical insulation, high-temperature resistance, and low thermal expansion, have become essential base materials in high-end fields such as power semiconductors, optoelectronic packaging, microwave radio frequency, and new energy storage. However, ceramics are inorganic materials bonded by ionic/covalent bonds, while metals are conductive materials with metallic bonds—creating a natural barrier in both physical properties and interfacial characteristics between the two. As a critical process for achieving reliable connections between ceramics and metals, ceramic metallization has long faced multiple technical bottlenecks in materials, interfaces, processes, and reliability. These challenges directly affect the yield and long-term service stability of ceramic substrate products including DBC, AMB, DPC, Mo-Mn thick film, and HTCC. This article systematically dissects the full-process technical pain points of ceramic metallization from four major dimensions—material essence, interfacial bonding mechanisms, process control, and end-application reliability—summarizes the root causes of these contradictions, and presents real-world cross-industry case studies to visualize both the technical value and engineering difficulties.

I. Material Essence: Inherent Physical-Chemical Conflicts Between Ceramics and Metals
The root of all difficulties in ceramic metallization lies in the inherent physical and chemical differences between these two material classes—an unavoidable intrinsic constraint.
1. Severe Coefficient of Thermal Expansion (CTE) Mismatch
Ceramics such as alumina (Al₂O₃), aluminum nitride (AlN), and silicon nitride (Si₃N₄) exhibit extremely low CTE values, while conductive metals like copper, nickel, and silver have CTE values several times higher. During the cooling stage after high-temperature sintering or brazing, the differential contraction rates continuously accumulate substantial residual thermal stress at the interface. This issue is particularly prominent in thick-copper DBC, AMB copper-clad substrates, and large-format ceramic substrates, directly leading to substrate warpage, ceramic cracking, metal layer peeling, and interfacial delamination failure after thermal cycling.
2. Chemically Inert Ceramic Surfaces Resist Wetting by Molten Metals
Ceramics rely on ionic and covalent bonds, giving them extremely low surface chemical activity. Molten solder or liquid metals cannot directly wet or spread on their surfaces, making physical adhesion unattainable. The industry generally introduces active transition metal elements such as Ti and Cr, which react with ceramics at high temperatures to form intermediate phases (e.g., titanates, aluminates) that build bridging bonds. Without such active transition layers, the adhesion between the metal layer and the ceramic approaches zero, and even slight external force can cause peeling.
3. Porosity and Surface Defects in Ceramics Introduce Hidden Risks
Conventionally sintered ceramics often contain microscopic pores and uneven surface roughness, giving rise to multiple quality risks: molten metal can infiltrate pores during high-temperature metallization, creating internal microcracks that accelerate propagation under stress; gases trapped in pores may be released during subsequent packaging, causing hermeticity failures; and in electroplating, voids can form in the plated layer, increasing adhesion variability and reducing batch-to-batch consistency.
II. Interfacial Bonding: The Most Critical Microstructural Control Challenge Across the Entire Process
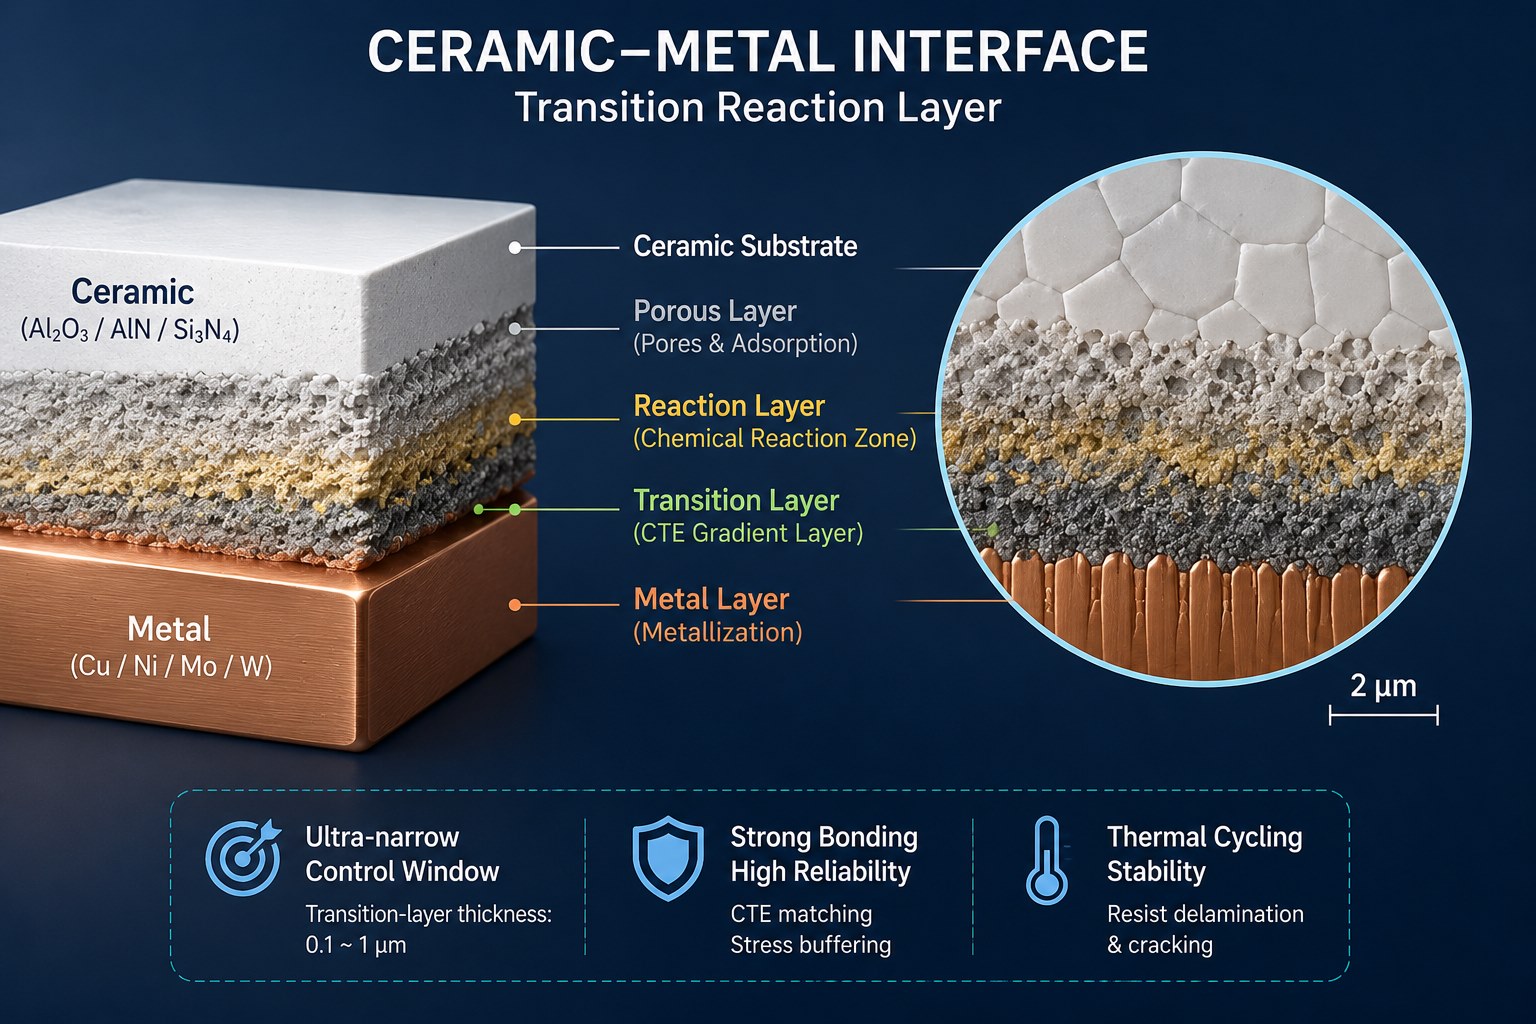
The bonding strength between ceramics and metals depends heavily on the microscopic interfacial reaction layer, whose parameters allow very little tolerance—this is widely recognized as the industry's core technical barrier.
1. Difficulty in Precisely Controlling Interfacial Chemical Reactions
The essence of metallization bonding lies in forming stable solid solutions or ceramic intermediate phases (e.g., titanates, aluminates) at the interface. The reaction outcome is highly sensitive to sintering temperature, atmosphere, and holding time. Slight fluctuations can cause two extreme failure modes: insufficient reaction yields too little intermediate phase, resulting in poor adhesion and easy peeling of the metal layer; excessive reaction generates excessive brittle compounds, reducing interfacial toughness and causing brittle fracture under thermal cycling, thereby degrading thermal-cycle resistance.
2. Extremely Narrow Thickness Window for Transition Layers
The industry commonly uses Ti, Mo, Mn, etc., as base transition layers, and thickness directly determines bonding performance: if the transition layer is too thick, overall brittleness increases and impact resistance drops; if too thin, a continuous and complete reactive bridge cannot form, leading to adhesion loss. Transition layer thickness is typically controlled at the nanometer-to-micrometer scale, making uniformity across the entire board and batch-to-batch consistency extremely challenging. Minor thickness variations can cause performance divergence among substrates from the same batch.
3. Interlayer Compatibility Issues in Multi-Layer Metal Stacks
Mature processes adopt multi-layer metal structures: an active base layer (Ti/Cr/Mo) + a diffusion barrier layer (Ni) + a solderable top layer (Cu/Au/Ag). At high temperatures, elemental interdiffusion and mutual dissolution occur among layers, forming brittle intermetallic compounds. This ultimately leads to blistering, delamination, or solder joint detachment in bulk failures.

III. Process Control: Extremely Low Tolerance Across All Manufacturing Steps
From high-temperature sintering and pattern formation to electroplating and post-treatment, every process step has a very narrow operating window. Minute fluctuations in equipment, environment, or raw materials can cause large-scale rejections.
1. Very Tight Control Ranges for Sintering Atmosphere and Temperature
Different technology routes impose strict requirements on temperature zones and atmospheres, with minimal permissible deviations: Mo-Mn thick-film and HTCC processes require a hydrogen-nitrogen weak reducing atmosphere, and temperature fluctuations exceeding ±10°C can alter adhesion and hermeticity; the copper-oxygen eutectic reaction window for DBC (direct bonded copper) is extremely narrow, and even trace variations in oxygen content in the furnace can cause weak bonding or copper-layer over-oxidation; AMB (active metal brazing) relies on high vacuum, and imbalances in temperature profiles or ramp rates can directly induce ceramic cracking.
2. Difficulties in Pattern Precision and Edge Consistency
Thick-film printing, DBC, and AMB processes are prone to line burrs, bleeding, open circuits, and line-width deviations. Although DPC (direct plated copper) thin-film processes offer higher precision through photolithography and sputtering, they demand stringent equipment accuracy and cleanliness, leading to elevated production costs. For high-power and high-frequency devices, stringent requirements on line width, spacing, and metal-edge verticality mean that pattern defects directly reduce manufacturing yield.
3. Plating Stress and Pinhole Defects in Electroplating
After metallization, nickel/gold plating is required to achieve solderability. Two typical defects commonly arise during electroplating: excessive internal stress in the plated layer, which pulls on the underlying metal and causes warpage or delamination; and pinholes or localized missing plating due to surface contamination or micropores, leading to poor soldering and reduced corrosion protection in later stages.
4. High-Temperature Deformation of Large, Thin Ceramic Substrates
Current mainstream power-device ceramic wafers are only 0.25–0.6 mm thick, while demand for large-format substrates continues to grow. After high-temperature metallization, warpage, bowing, or waviness frequently occurs. If deformation exceeds tolerance, subsequent die-attach and assembly become impossible, resulting in direct scrap.
IV. Reliability and End-Use Applications: Stringent Tests in Service Environments
Ceramic-metallized substrates must operate long-term under harsh conditions including thermal cycling, vacuum sealing, and high-frequency bonding. Achieving consistent reliability in mass production remains the greatest engineering challenge.
1. Interfacial Fatigue Failure Under Thermal Cycling and Thermal Shock
Power devices typically operate over -40°C to 125°C. Under repeated long-term cycling, stresses caused by CTE mismatch continuously alternate, gradually leading to metal-layer fatigue, interfacial microcracking, and ultimately complete delamination—this is the most common failure mode in mass-produced power devices.
2. High-Hermeticity Packaging: Inspection and Control Difficulties
Microwave waveguides, laser devices, and vacuum hermetic packages impose extremely stringent leak-rate requirements. Micro-cracks or gaps invisible to the naked eye require specialized leak-detection equipment. Any microscopic interfacial defect can cause product leakage failure, making full-process defect control highly challenging.
3. Inconsistent Wire-Bonding and Soldering Performance
The surface roughness, oxidation level, and plating thickness uniformity of the metallization layer directly affect downstream packaging processes: insufficient pull strength in gold/aluminum wire bonding leads to bond lift-off; poor wettability in SMT soldering causes cold joints, significantly reducing packaging yield.
4. Poor Batch-to-Batch Consistency, Difficulty in Improving Mass-Production Yield
The final performance of ceramic metallization is affected by multiple coupled factors—ceramic green-body batch variation, metal paste composition, furnace temperature profiles, and workshop cleanliness. Fluctuations in any single parameter can cause adhesion scatter, cracking, gas leakage, or other defects. Achieving stable yield in large-scale production remains a long-standing engineering challenge.
V. Summary of Root Causes of Technical Challenges
Synthesizing the full-process pain points, all technical bottlenecks in ceramic metallization can be distilled into three core root causes:
· Inherent physical contradiction — The intrinsic mismatches in CTE and chemical bonding between ceramics and metals cannot be fully eliminated at the material level; stress and wetting issues are fundamentally unavoidable.
· Microscopic interfacial uncontrollability — Interface reactions, transition-layer thickness, and multi-layer metal diffusion all occur at the microscale, where precise parameter control is highly difficult, and minor fluctuations significantly alter bonding strength.
· Narrow process windows combined with stringent reliability standards — Sintering temperature, atmosphere, ramp rates, etc., have very low fault tolerance; simultaneously, end-use requirements for thermal cycling, hermeticity, wire bonding, and soldering multiply the constraints, amplifying process-control difficulty.
VI. Core Industry Application Case Studies
As a foundational enabling technology for high-end electronics manufacturing, ceramic metallization is widely applied in communications, power semiconductors, optoelectronics, medical devices, automotive, and aerospace sectors. Each scenario adopts differentiated process routes to address core needs such as insulation and heat dissipation, hermetic packaging, and high-frequency transmission, while directly reflecting the interface-control and process-stability challenges discussed above. All case parameters have been calibrated against industry-standard specifications and mass-production inspection protocols to ensure data rigor and traceability.

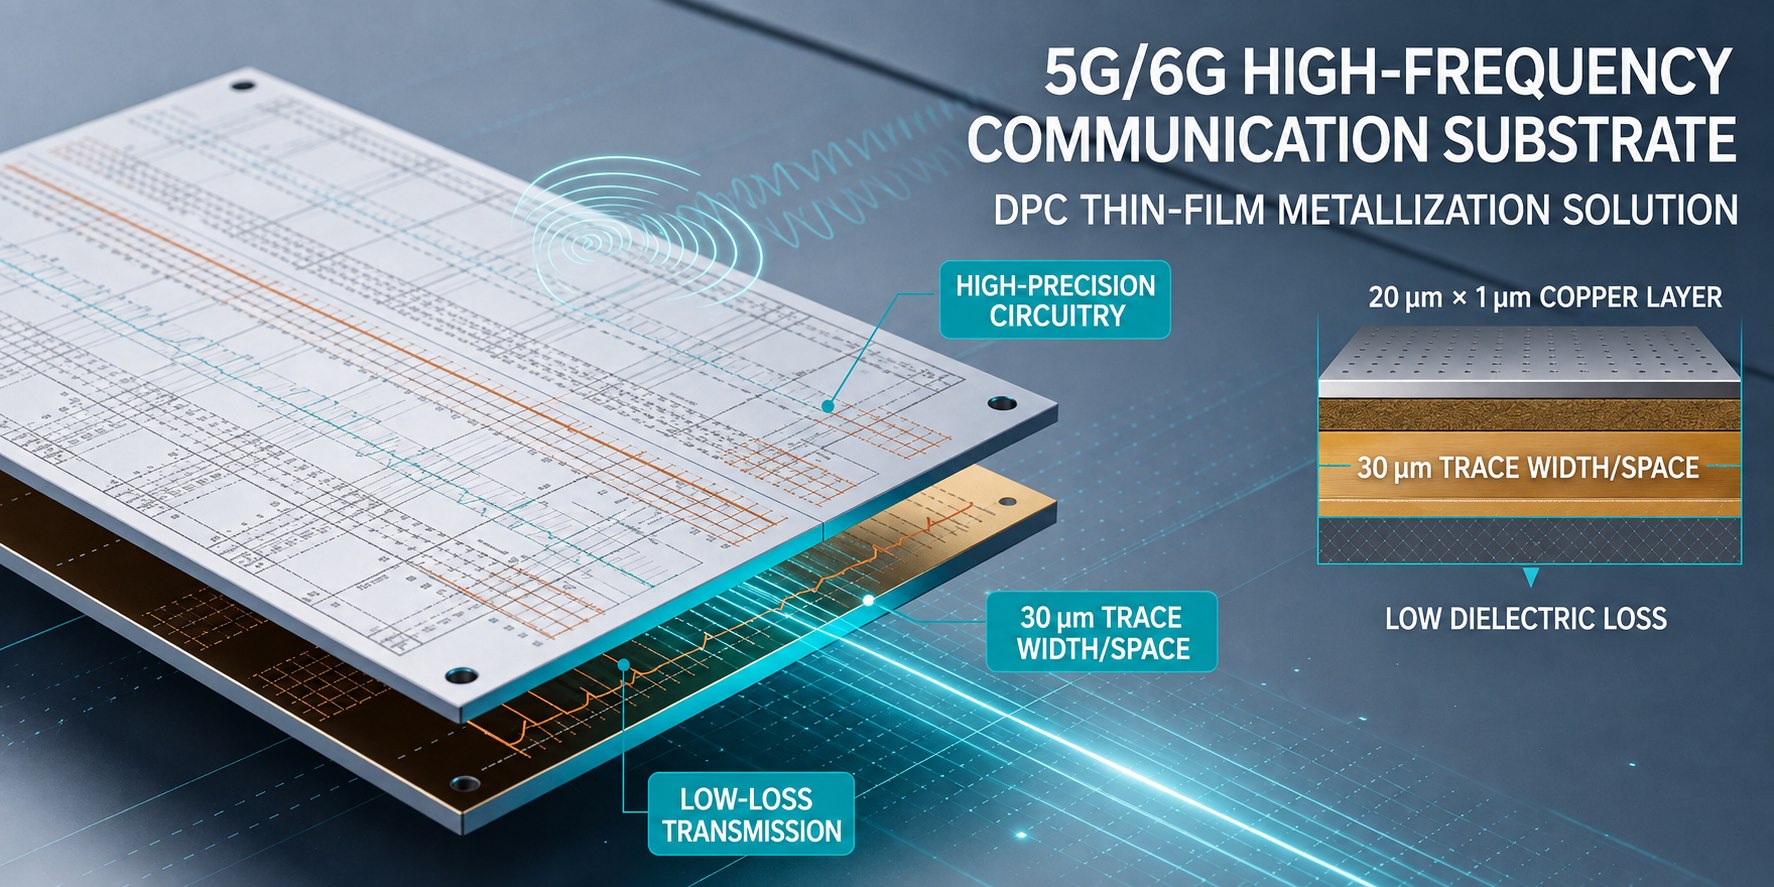
1. High-Frequency Substrates for 5G/6G Communications (DPC Thin-Film Metallization)
5G macro base stations and high-speed optical transceivers demand high-frequency, low-loss, high-precision circuitry, and excellent thermal dissipation—areas where traditional organic PCBs fall short due to high losses and poor heat resistance. Using a self-developed high-precision DPC thin-film metallization process, Kinji Group has commercialized aluminum-nitride ceramic substrate solutions. Through magnetron sputtering, a high-purity copper conductive layer with thickness of 20 μm ±1 μm is precisely deposited onto the AlN substrate, achieving stable 30 μm ultra-fine line/space patterning. Low dielectric loss effectively reduces high-frequency signal attenuation and controls temperature rise. With 36 standardized quality-control steps throughout the process, plus nickel-palladium-gold post-plating, defects such as pinholes, oxidation, and thickness non-uniformity are eliminated, ensuring that electrical performance variation stays below 1% under long-term high-frequency operation—fully meeting the reliability requirements of 5G baseband modules and high-speed optical transmission equipment.
2. New-Energy Vehicle Power Module Applications (AMB Active Metal Brazing)
Power devices in EV electronic control units, OBCs, and photovoltaic inverters operate under -40°C to 125°C alternating thermal conditions, high vibration, and heavy loads, demanding exceptional thermal-shock and delamination resistance. Kinji Group has developed a low-temperature AMB process tailored for automotive applications and launched silicon-nitride ceramic AMB metallized substrates. By precisely controlling vacuum sintering zones, maintaining constant vacuum, and standardizing ramp/soak profiles, excessive formation of brittle compounds is suppressed, while interfacial stress matching and bond toughness are optimized. The copper-to-ceramic interfacial bonding strength reaches 85 MPa, far exceeding the industry average of 62 MPa. In authoritative automotive reliability tests, mass-produced substrates reliably pass 1,000+ (and up to 2,000+ for upgraded versions) -40°C to 125°C thermal cycles without delamination, cracking, or metal-layer peeling. These substrates are now in volume production for power modules used by leading domestic automotive and energy-storage companies.
3. High-Power Laser and Optoelectronic Packaging (Mo-Mn Thick Film + AuSn Eutectic Metallization)
Industrial high-power lasers, high-speed optical modules, and automotive LiDAR BAR chips require ceramic carriers with stringent hermeticity, low thermal resistance, and long-term high-temperature endurance. Leveraging mature Mo-Mn thick-film technology, Kinji Group provides a 96% alumina ceramic metallization solution for the TRUMPF 3 kW industrial semiconductor laser project. By precisely controlling the hydrogen-reduction sintering atmosphere, temperature, and holding time, a uniform and dense transition interface is formed, ensuring adhesion and hermeticity compliance. The substrate, combined with AuSn eutectic soldering, achieves overall thermal resistance ≤0.3 K/W, withstands localized high-temperature heat concentration from the laser, and resolves interfacial debonding and power degradation issues. Through continuous optimization of paste formulation and sintering parameters, metallization-layer adhesion is stably ≥5 N/cm, with batch fluctuation within ±0.2 N/cm. Production yield ranks among the industry's highest, and the solution is now in volume production for 10 Gbps optical modules and industrial laser equipment.
4. High-End Medical Precision Devices (Alumina Ceramic Hermetic Metallization)
Implantable medical devices and advanced diagnostic imaging equipment demand insulation, corrosion resistance, biocompatibility, and hermeticity at medical-grade standards. For implantable devices such as pacemakers and cochlear implants, Kinji Group custom-developed 96% alumina Mo-Mn hermetic packaging substrates. Using high-precision high-temperature sintering, defect-free metallized sealing layers are produced, achieving reliable electrical isolation between internal circuits and human tissue. Medical-grade hermeticity testing shows stable leak rates ≤1×10⁻⁸ mbar·L/s, resisting long-term bodily fluid penetration and preventing internal oxidation/corrosion. The products have passed biocompatibility and high-temperature sterilization tests, adapting to MRI, CT, and other high-frequency electromagnetic radiation environments, as well as repeated sterilization cycles, without deformation, leakage, or aging issues. They have become a core domestic substitute product for high-end medical electronic components.
5. Aerospace and Industrial High-End Equipment Applications
Aerospace airborne radar, engine temperature-sensing assemblies, and advanced plasma coating equipment impose extreme requirements on high-temperature resistance, aging resistance, and environmental stability of ceramic-metallized components. Leveraging its full-process matrix of HTCC, LTCC, DBC, and AMB technologies, Kinji Group precisely addresses these demanding scenarios. Its mass-produced HTCC thick-film metallized substrates withstand 1,000°C short-term thermal shock while maintaining signal stability, interfacial integrity, and dimensional accuracy under vacuum, strong electromagnetic interference, and alternating temperature environments. Addressing the common electrode wear issue in industrial plasma coating equipment, Kinji developed a silver-palladium-system ceramic metallized electrode that overcomes the limitations of conventional pure-metal electrodes—high-temperature oxidation and wear. The working-surface wear rate is reduced by 35%, extending continuous service life from 3 months to over 5 months, significantly cutting maintenance costs and offering a preferred solution for domestic upgrading of high-end equipment.
Conclusion
Ceramic metallization is the key bridge connecting ceramic insulating substrates and metallic conductive circuits, with technical challenges spanning the entire chain of materials, interfaces, processes, and reliability. From 5G/6G high-frequency communications and new-energy automotive power terminals, to high-power laser optoelectronics, advanced medical devices, and aerospace applications, these standardized case studies demonstrate that precise interfacial control, process stability, and stress-matching capability directly determine the performance ceiling, yield, and long-term service life of high-end electronic devices. As third-generation semiconductors, new-energy storage, and high-speed optical interconnect industries rapidly evolve, demand continues to grow for large-format, ultra-thin, high-precision, and high-reliability ceramic substrates. How to fundamentally balance material physical contradictions, achieve microscopically precise interfacial control, and broaden stable mass-production process windows will remain the core R&D directions for the ceramic packaging materials industry in the years ahead.
trending news
Contact Us